+44 (0)161 339 3049

Case Studies

Explore our Case Studies to see how ThermTech has helped clients worldwide improve energy efficiency, reduce operational costs, and lower emissions through custom-designed heat recovery and gas cooling systems.
Customer required an economiser to fit into existing space. Thermtech designed it to slot perfectly onto existing connections, minimising production downtime.
Customer’s existing hot-well was leaking and deemed unsafe, Thermtech provided a replacement. The area was very tight and the existing tank and new hot-well had to come in and out through the roof.
Customer required the Installation of economsiers on each of their 2-off 10,000Kg/Hr rated Boilers to reduce gas costs. The boiler house had minimum space so Thermtech designed an economsier to fit onto the back of the boiler smokebox, making the most out of the space available.
Customer wanted to increase the efficiency of their 5,700 Kg/hr Rated Steam Boiler and reduce gas costs, Thermtech Installed a retro-fit Boiler Economiser and updated the pipeworks and boiler level controls for maximum efficiency.
Customer required replacement hot-well due to existing unit leaking, the hot-well was located high up on a mezzanine floor with no easy access for removal and installation. The dowtime to complete the works was 1 week.
Customer was looking to utilise waste heat coming from a 388kW gas fired hot-water boiler, Thermtech designed a small heat exchanger to recover waste heat from the flue gas to generate further hot water which can be used for process purposes.
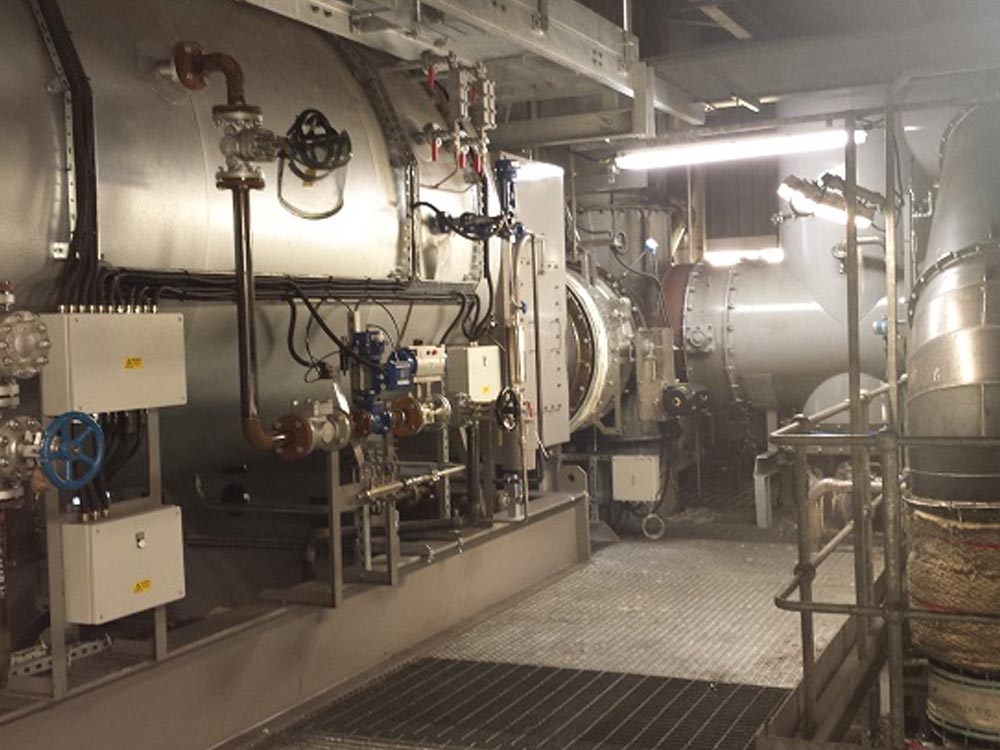
The waste heat boiler economiser is designed to cool the incinerator exhaust gases exhausted from the waste heat boiler from 206 °C down to 136 °C, thereby preheating the boiler feed water from 80 to 150°C, recovering ~700 kW of waste heat.
A UK-based dairy product manufacturing plant generates a percentage of its overall steam output with 2x 8,000 kg / hr rated wood chip fired steam boilers. Bespoke design to suit the individual boiler system.
Customer required design, manufacture, and delivery of Chemical storage vessels.
Customer required replacement of damaged dampers and filter transitions.
Customer needed two-off Large Economisers manufactured with a quick turnaround.
Replacement of existing damaged economiser, with new Thermtech economiser.
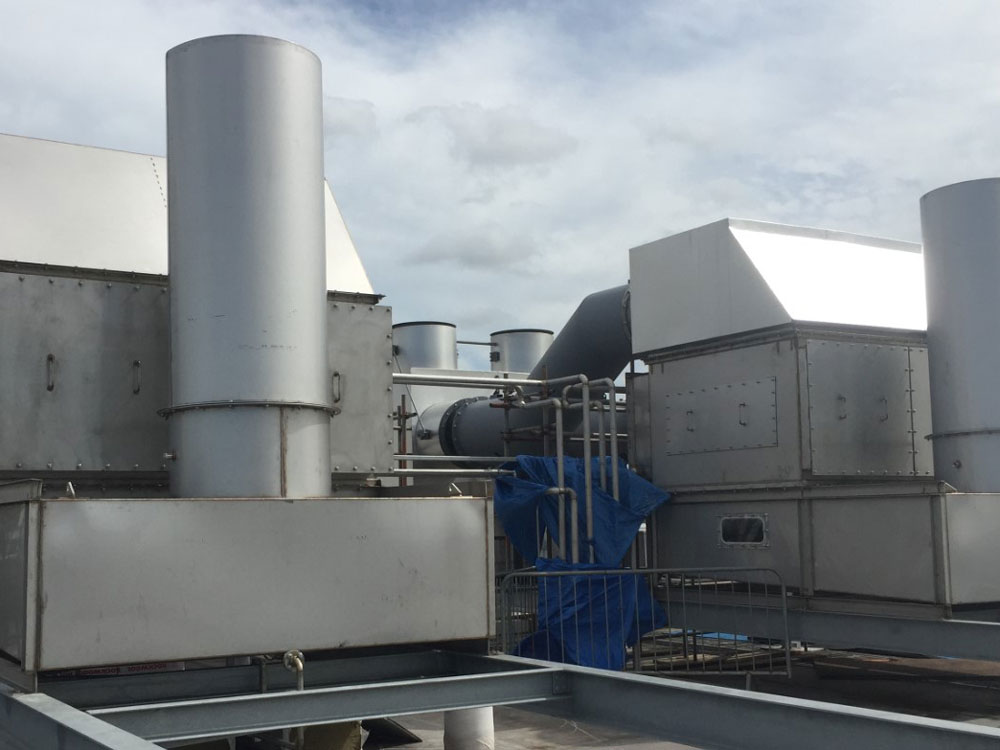
When a UK-based textiles manufacturing plant were looking to increase the energy efficiency of its twin yarn drying process lines ThermTech designed, manufactured, and installed a waste heat recovery system which met their needs.
ThermTech were appointed to design a waste heat recovery system which would improve efficiencies at the plant for a UK-based edible oils processing plant uses activated carbon in order to clean up various contaminants contained within the oils for product quality reasons.
ThermTech were asked to design, manufacture, and retrofit two bespoke steam boiler economisers to the boilers for a UK based specialty chemicals production facility to help further improve the energy efficiency of the site.
When Noble’s Hospital on the Isle of Man was looking to reduce operating costs ThermTech designed, manufactured, and retrofitted three bespoke boiler economisers to help them do this.
A UK-based edible oils processing plant uses activated carbon in order to clean up various contaminants contained within the oils for product quality reasons.
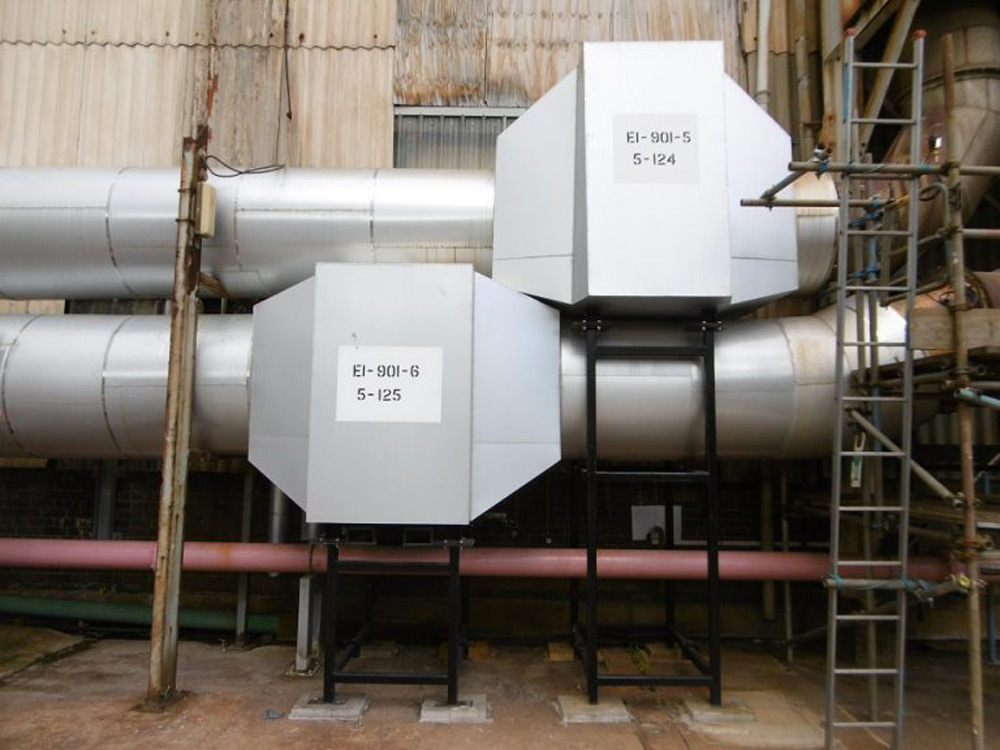
An Electrostatic Precipitator is an extremely energy efficient abatement solution for oily smoke fumes using only 30 watts/1000m3/hour, compared to an incinerator at 3KW/1000m3/hr.